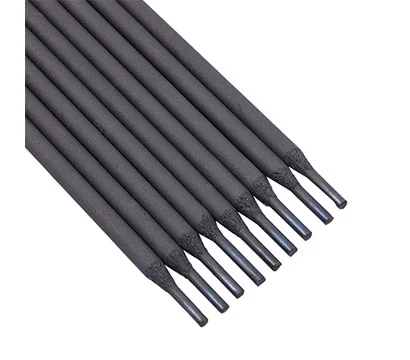
Z308 PRODUCT DATA Z308 Nickel Welding Rod Quick Specifications
Key specification and application information for Minghua Z308 pure-nickel-type cast iron welding electrode.
| Trade Designation | Z308 |
| AWS Classification Reference | ENi-CI under AWS A5.15, subject to confirmation by the applicable Minghua TDS or certificate |
| Chinese Standard Reference | GB/T 10044-2022 ; confirm the exact classification on the product certificate |
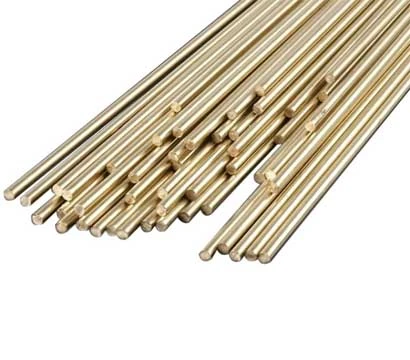
| Product Type | Pure-nickel-type covered cast iron electrode |
| Welding Process | SMAW / MMA / Stick welding |
| Minghua Polarity | AC or DC+ |
| Available Diameters | 2.5 mm, 3.2 mm, 4.0 mm and 5.0 mm |
| Example Deposited Nickel | 93.2% |
| Primary Application | Repair welding of gray cast iron components |
| Key Characteristic | Machinable deposited weld metal |
Classification Note:
Z308 is commonly cross-referenced to the ENi-CI pure-nickel cast iron electrode type. Confirm classification, composition and compliance requirements through the TDS or certificate supplied with the ordered product.
Features of Z308 Nickel Welding Rod
Pure Nickel Core Wire Designed for cast iron repair applications where a high-nickel deposited weld metal is required.
Machinable Weld Deposit Suitable for repaired areas that may require drilling, milling, tapping, grinding or other post-weld machining.
Suitable for Gray Cast Iron Repair Commonly selected for gray cast iron components where repair accuracy, machinability and control of hard brittle weld zones are important.
AC or DC+ Operation Minghua product data permits AC or DC+ operation within the applicable current range.
Multiple Diameter Options Available in 2.5 mm, 3.2 mm, 4.0 mm and 5.0 mm diameters for different repair dimensions and welding-current requirements.
Z308 SELECTION Why Choose Z308 for Machinable Cast Iron Repair?
Z308 is particularly valuable where the repaired cast iron component must be machined after welding. Its high-nickel deposit helps provide a relatively soft, machinable weld area compared with harder cast iron repair deposits.
Machinability After Welding — useful for repair areas that require milling, drilling, turning, tapping or grinding.
Gray Cast Iron Compatibility — commonly selected for repairable gray iron castings when the repair procedure permits a pure-nickel-type electrode.
Precision Repair Applications — relevant for machine-tool components, housings, guideways and similar cast parts requiring dimensional restoration.
Z308 Example Deposited Weld Metal Composition
The following values are Minghua example deposited-weld-metal data for this product. They should not be interpreted as universal classification limits or as a replacement for the applicable batch certificate.
| Example Chemical Analysis of Deposited Metal (%) |
| Test Item | C | Mn | Si | S | Ni | Fe |
| Example Value | 1.45 | 0.85 | 1.8 | 0.003 | 93.2 | 2.15 |
Buyer Note: Request the applicable TDS and batch certificate when the project requires verified chemical composition, classification or inspection documentation.
Minghua Reference Current for Z308 Electrode
| Recommended Current for Z308 Cast Iron Electrode – AC or DC+ |
| Electrode Diameter | 2.5 mm | 3.2 mm | 4.0 mm | 5.0 mm |
| Reference Current | 60–100A | 90–120A | 130–180A | 160–190A |
These values are Minghua reference settings rather than fixed production parameters. Final current and polarity depend on electrode diameter, welding position, casting condition, joint preparation and the approved repair procedure.
What Is Z308 Nickel Welding Rod Used For?
Z308 nickel welding rod is primarily used for repair welding of gray cast iron components when machinability, crack control and repair accuracy are important. Final suitability should be determined according to cast iron grade, casting condition, restraint, service load and the approved repair procedure.
Engine Blocks & Cylinder HeadsRepair of suitable gray cast iron cracks, worn areas and localized casting defects after material and damage assessment.
Machine Tool Beds & GuidewaysRepair of precision cast iron surfaces that may require machining after welding.
Pump HousingsRepair of cracks, worn sealing areas and localized defects in compatible gray cast iron housings.
Gearboxes & Equipment HousingsLocal restoration where dimensional accuracy and post-weld machinability are required.
Foundry DefectsRectification of selected pores, cracks and localized casting defects before final machining.
Thin or Machined Cast Iron SectionsRepair applications where a relatively soft and machinable high-nickel deposit is preferred.
Z308 vs Z408 vs Z208: Which Cast Iron Electrode Fits the Repair?
Z308, Z408 and Z208 serve different cast iron repair requirements. The table below provides a short product-selection summary only; detailed comparison belongs in the dedicated selection guide.
| Product | General Type | Typical Positioning | Selection Focus |
|---|
| Z308 Nickel Welding Rod | Pure-nickel-type cast iron electrode | Gray cast iron, machined surfaces and repairs requiring machinable weld metal | Prioritize when weld machinability and repair accuracy are important |
| Z408 Cast Iron Welding Rod | Nickel-iron-type cast iron electrode | More highly restrained, thicker or higher-load cast iron repairs | Consider where the repair requires a nickel-iron electrode and higher deposited-metal strength |
| Z208 Cast Iron Welding Rod | Economical cast iron repair electrode | General or cost-sensitive cast iron maintenance | Use only when its weld-metal properties and machinability meet the repair requirements |
Basic Guidance for Using Z308 in Cast Iron Repair
Product selection and welding procedure are separate decisions. Cast iron repair is sensitive to contamination, thermal stress and casting restraint, so the points below are general principles rather than a replacement for a qualified repair procedure or WPS.
1. Identify the Casting and Damage
Confirm cast iron type, crack extent, restraint and expected service load before choosing the repair method.
2. Clean the Repair Area Thoroughly
Remove oil, paint, moisture, rust, scale and contaminated surface material before welding.
3. Match Diameter and Current
Select electrode diameter and current according to casting thickness, welding position and repair dimensions.
4. Control Heat Input
Short beads or intermittent welding may be used where required by the repair procedure to limit local heat input and shrinkage stress.
5. Control Cooling
Follow the approved procedure for preheat, interpass temperature and cooling. Avoid uncontrolled rapid temperature changes.
Preheat Note:
There is no single preheat rule for every cast iron repair. Cold-welding and preheated procedures may both be appropriate depending on casting size, material grade, restraint, crack condition and the approved repair method.
FAQ About Z308 Nickel Welding Rod
What is Z308 nickel welding rod used for?
Z308 is primarily used for repair welding of gray cast iron components requiring machinable deposited metal. Typical applications include suitable engine blocks, cylinder heads, machine bases, guideways, pump housings, gearboxes and selected foundry defects.
What does Z308 electrode mean?
Z308 is a trade designation commonly used in China for a pure-nickel-type covered electrode intended for cast iron repair. International classification and compliance should be confirmed through the applicable product TDS or certificate.
Is Z308 equivalent to AWS ENi-CI?
Z308 is commonly cross-referenced to the ENi-CI pure-nickel cast iron electrode type under AWS A5.15. Buyers should confirm the supplied classification through the Minghua TDS or certificate for the ordered product.
Is Z308 suitable for welding gray cast iron?
Yes. Z308 is primarily positioned for gray cast iron repair, particularly when weld machinability and crack control are important. Final suitability depends on casting condition, restraint and the approved repair procedure.
Is Z308 deposited weld metal machinable?
Z308 is selected where a relatively soft and machinable high-nickel deposit is required. Actual machinability depends on dilution, heat input, welding technique and the condition of the base casting.
Can Minghua Z308 welding rod be used with AC and DC?
Minghua product data lists AC and DC+ operation. Use the applicable current range and confirm the required power-source setting through the product TDS and approved repair procedure.
What is the recommended current for Z308 welding rod?
Minghua reference values are 60–100A for 2.5 mm, 90–120A for 3.2 mm, 130–180A for 4.0 mm and 160–190A for 5.0 mm electrodes. Final settings depend on welding position, casting thickness and repair procedure.
What is the difference between Z308 and Z408?
Z308 is a pure-nickel-type electrode commonly selected when machinability is important, while Z408 is a nickel-iron-type electrode used for different repair conditions where deposited-metal strength and casting restraint may be more important. Final selection should follow the repair requirements.
What information is required for a Z308 quotation?
Provide the required electrode diameter, quantity, packaging, destination and certificate requirements. Information about cast iron grade, repair component and post-weld machining requirements is also useful.
PRODUCT INQUIRY Need Z308 Nickel Welding Rods?
Send Minghua your required diameter, quantity, packaging, cast iron application, destination and certificate requirements for product confirmation and quotation.
Request a Z308 Quote